-
-
Phone
+86-13623462298




The procedure for assembling flange connections 2026: RF standards - Plants
2026-07-28
Let's be clear: if you're looking for a relevantassembly procedure for flange connectionsto simply “hand over the facility to technical supervision” in 2026, this article may disappoint you. I will not retell the dry points of GOST that lie on your table in the form of dusty brochures. We will talk about how these standards work (or don’t work) in the real conditions of Russian factories, where the frost is minus forty, deadlines are running out, and Western seals disappeared from warehouse shelves two years ago. A quiet revolution is now taking place in the industrial sector of the Russian Federation: we are forced to rewrite the rules of the game, because the old instructions were written for different materials and a different production culture.
Why the old GOST is bursting at the seams in the realities of 2026
Have you noticed how often micro leaks appear on new objects after hydraulic tests? It would seem that everything was done by the book. The tightening torque is maintained, the gasket is installed, and the surface is cleaned. But the system “flows”. The problem lies in the fundamental discrepancy between the regulatory framework, which is updated with difficulty, and the real materials available on the Russian market today.
Previously, about five to seven years ago, an engineer could simply indicate in the specification a paronite or a spiral wound gasket (SNG) from a well-known European brand, and the issue was closed. Today? Today the market is filled with products that formally meet the declared characteristics, but behave unpredictably under cyclic loads. This is especially true for high-temperature components.
I personally observed the situation at one of the oil refineries in the Volga region in the winter of 2025. The team assembled the flange connection strictly according to the regulations, using new Russian analogues of imported gaskets. The pressure was kept for a day - everything was clear. We started the process, temperature expansion began. Three days later - a whistle. The reason is simple: the coefficient of thermal expansion of the new composite material was not taken into account in the old method of calculating the tightening force. There are standards, but adaptation to new materials is not.
This is the main challenge of 2026.Assembly procedure for flange connectionsceased to be a mechanical action of “tightening the nut all the way.” This is now an engineering problem that requires an understanding of the chemistry of materials and the physics of processes. If you continue to assemble components the way you were taught at the institute in 2010, you risk an emergency shutdown of production.
Breaking changes in sealing approaches
What exactly has changed? Firstly, control over the flatness of the flanges has been tightened. Previously, small risks or scratches were allowed, which were “clogged” with a soft pad. With the transition to more rigid and chemically resistant, but less plastic materials, any surface defects become critical. Factories are introducing mandatory metrological control of flange mirrors before assembly. This is not a whim, it is a necessity.
Secondly, the tool. Hydraulic impact wrenches have become the standard even for diameters where previously wrenches and pipe “extensions” were used. Why? Because the human factor in the matter of tightening uniformity has become too expensive. An installer's mistake in turning a corner costs more than renting a set of equipment.
But the most interesting thing is hidden in the fastening details. Studs and bolts. It would seem, what is there to change? Metal is metal. But no. In the context of import substitution, a flood of fasteners of dubious quality has poured onto the market. Externally - shiny, there are markings. In fact, the yield strength is lower than stated, or uneven hardening. When tightened, such a bolt can imperceptibly “float”, creating the illusion of a normal torque, and after a week weaken under load.
Therefore, the modern assembly procedure begins not with installation, but with incoming inspection of each batch of hardware. Sounds bureaucratic? Maybe. But the alternative is a torch on the installation.
Technological map: how to collect correctly under current conditions
Let's take a step-by-step look at what a competent assembly process looks like in 2026, taking into account all the nuances of the Russian climate and logistics. Forget about linear instructions. What is important here is consistency and control of each stage.
Preparation: The Step Everyone Ignores
90% of problems with tightness start here. The installers are in a hurry. They need to hand over the volume. They quickly clean off the rust with a brush, wipe it with a rag and install a gasket. This is a recipe for disaster.
Correct algorithm:
- Visual and instrumental control.Checking flatness with a feeler gauge. If there is a screw mark from an old tool, grind it. The depth of the marks should not exceed the permissible values for a specific type of gasket. For soft materials the requirements are softer, for graphite or PTFE - stricter.
- Cleaning the threads.This is critical. Rust or dirt in the threads will change the coefficient of friction. You turn the nut with the right torque, but 40% of the force is spent on overcoming friction in the dirt, and not on compressing the gasket. The result is unattainable. Use special thread cleaners, not diesel fuel, which leaves a film.
- Lubrication.Only specialized lubricants with a known friction coefficient. No “Litol” or working off! The friction coefficient must be recorded in the assembly passport. The recalculation of the tightening torque depends on this. In winter in Siberia, ordinary grease freezes, turning into an abrasive. We need frost-resistant compounds that work down to -60°C.
Alignment and gasket installation
Never use the gasket as a centering element! This is a grave mistake. The flanges must be aligned before installing the seal. If you try to tighten warped flanges with the force of the bolts, you create a bending moment in the stud. It will work on fracture, not tension. Fatigue failure of such a bolt is a matter of time.
The gasket must fit freely. If it is tight, there is something wrong with the dimensions or alignment. Pay attention to the installation direction of the spiral wound gaskets. There is an internal restrictive ring. It cannot be placed upside down, otherwise, at the first increase in pressure, the gasket will be squeezed inside the pipeline (“jam effect”). Many factories now mark the outside of the gasket with paint to prevent the installer from confusing the orientation.
Tightening process: criss-cross is no longer enough
The good old criss-cross method is good for small diameters and low pressures. For critical units DN 100 and above, in 2026 a multi-pass design with rotation angle control or hydraulic tension will be used.
Action plan:
- Pre-tightening by hand.Make sure all nuts are loose.
- First pass (30% effort).Tighten in a circle (not in a cross!) to evenly press the gasket without distortion.
- Second pass (60% effort).Classic cross pattern for load balancing.
- Third pass (100% effort).Final tightening in a circle to stabilize.
- Control pass.After 15-30 minutes (after relaxation of the material), check the moment. Often a little tweaking is required.
An important nuance: when using hydraulic tensioners, the order changes. There we work in groups of bolts located diametrically opposite. This eliminates flange distortion even with large diameters.
Economics of the issue: prices, risks and commercial component
A conversation about technology wouldn't be complete without a discussion about money. Implementing the correct assembly procedure for flange connections is expensive. And many plant managers are trying to save money here, considering it “overkill.” Let's do the math.
A set of professional tools (hydraulic pump, heads, hoses) costs from 300,000 to 1,500,000 rubles, depending on the class and manufacturer (now high-end Chinese brands or remnants of European ones predominate). Staff training costs about another 50,000 rubles per person. High-quality lubricants and consumables add 10-15% to the estimate.
Does it seem like a lot? Compare this to the cost of an hour of installation downtime. At a large refinery or chemical plant, stopping a line due to a leak can cost millions of rubles per hour. Plus environmental fines, which have become really noticeable in Russia. Plus the risk of fire.
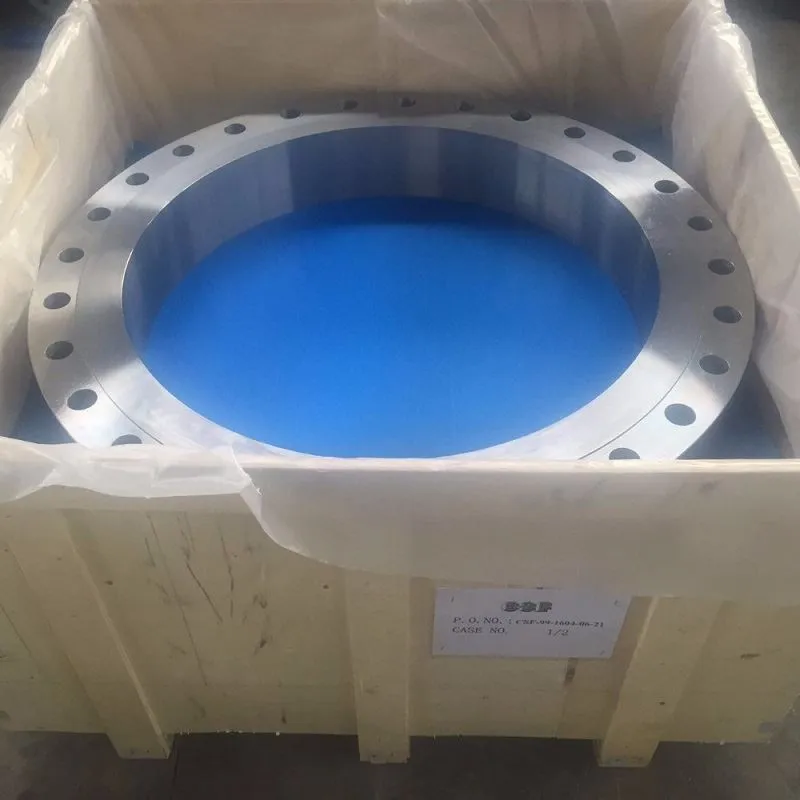
In this context, choosing a supplier for the basic elements—the flanges themselves—becomes a strategic decision. The market offers many options, but the reliability of the connection directly depends on the quality of the initial forging and compliance with the geometry. For example, a companyShanxi Hongkai Forging Co., Ltd., based in China's key industrial hub of Dingxiang County, demonstrates an approach that will become increasingly popular in 2026. With three in-house production sites covering the full cycle from forging to final packaging, they ensure vertical integration that eliminates intermediaries and reduces the risk of defects.
Their range covers six main types of forged flanges (from overhead to blind) ranging from DN15 to DN4000, which allows them to cover the needs of both compact units and main pipelines. It is important to note that the products are manufactured not only according to international standards (ASME, DIN, ANSI B16.5), but also strictly according to GOST specifications, which is critical for the Russian industry. Having the right to independently export simplifies logistics and makes interaction transparent. For engineers faced with the problem of the floating geometry of cheaper alternatives, this approach - with the manufacturer controlling heat treatment, machining and multi-level quality control at all stages - ensures that the flange does not become a weak link in a system assembled according to the new strict rules.
In 2026, an interesting trend is observed: service companies offer not the sale of tools, but the rental of kits along with a team of certified installers. This is beneficial for one-time repairs or commissioning work. The cost of such a contract varies from 50,000 to 200,000 rubles per shift, but includes a guarantee of tightness. If it leaks, they will repair it at their own expense. This relieves the customer of headaches.
It is also worth mentioning the cost of the gaskets themselves. Switching from cheap paronite to high-quality graphite or multilayer metal gaskets increases the cost of the unit by 3-5 times. But the service life increases 10 times. Skimping on gaskets is a classic false economy.
Comparison table: Traditional approach vs Modern standard 2026
| Parameter | Traditional Approach (Obsolete) | Modern Standard (Recommended) |
|---|---|---|
| Tool | Manual wrenches, mid-range torque wrenches | Hydraulic impact wrenches, smart dynamometers with memory |
| Force control | “By eye” or by one moment value | Multi-pass tightening with angle control and data fixation |
| Surface preparation | Cleaning with a rag, allowing minor defects | Metrological control of flatness, mandatory grinding |
| Lubrication | Universal lubricants (Litol, grease) | Certified mounting pastes with known friction coefficients |
| Documentation | Mark in the work log “completed” | Electronic passport of the unit with photo recording and data on each bolt |
| Implementation cost | Low | High (but pays off due to the absence of accidents) |
Hidden threats: what manufacturers are silent about
Now let’s move on to something that is rarely written about in advertising brochures. There is one problem that has become the scourge of Russian industry in the last two years. This is the “creep effect” of new composite materials.
In pursuit of import substitution, many factories began to produce their own analogues of foreign gaskets. The chemical composition seems to be the same. But pressing technology and fiber packing density are know-how. And this is where a puncture often happens. The material under load begins to slowly “flow” (creep). You tightened the flange, checked - everything is ok. A month has passed. The gasket became more compact than designed, and the force in the bolts dropped. A leak has appeared.
How to deal with this? The only working method is re-torquing after a certain period of operation. In the old standards this was mentioned in passing. In the new regulations of leading companies, this has become a mandatory point for certain classes of environments. If your contractor doesn't offer a guaranteed re-stretching service 48 hours after start-up, run away from them.
Another hidden enemy is stress corrosion. In aggressive environments (sulfuric acid, alkalis), the combination of residual stresses in the bolt and chemistry leads to sudden brittle failure of the fastener. The bolt breaks without warning. Solution? The use of bolts made of special grades of steel with protective coatings that actually work, and do not just create the appearance of protection. And regular ultrasonic inspection of bolt lengths to detect hidden cracks.
Human factor and qualifications
You can buy the best tool for millions, but if it is used by a person who does not understand the physics of the process, the result will be disastrous. In Russia, the shortage of qualified process pipeline installers has reached a critical level. Young people are not joining the edit industry, old people are leaving.
You can often see a picture at sites: a guy with a hydraulic pump simply presses a button, without paying attention to the skew of the head. Or he uses an extension cord to “finish off” a nut that the pump did not take. This discredits the very idea of mechanization.
In 2026, progressive factories will introduce a system of personal responsibility. Each bolt is marked with the installer's mark. If a year later a leak is discovered due to the lack of tension, the culprit is known. It's tough, but effective. The practice of video recording the assembly process is also gaining popularity. The camera records the entire tightening cycle, the data is saved in the archive. When debriefing after an accident, it is possible to determine exactly who violated the technology and how.
Forecast and unique expert opinion
Where are we going? I believe that in the next 3-5 years we will witness a complete abandonment of manual labor in the assembly of critical flange connections at large facilities. It's inevitable. The cost of a mistake will become too high.
But there is also another side to the coin. Excessive automation and bureaucratization of the process can lead to engineers losing their feel for the material. The device will show a “green light”, and the connection will leak due to a nuance that the machine did not see (for example, a microscopic chip at the end). Therefore, I insist: technology should help a person, and not replace his brain completely. An experienced craftsman who understands why a nut is tight is more valuable than any robot.
I also want to touch on the topic of standardization. Now in the Russian Federation there is a patchwork quilt of GOST, SNiP, STO of various companies and internal regulations. This creates confusion. We need a unified, modern national standard for the assembly of flange connections, which would take into account modern materials and climatic zones of Russia from Kaliningrad to Kamchatka. For now, each major player writes its own rules, which complicates the work of contractors working at different sites.
And the last piece of advice that can save your nerves and your budget: do not blindly trust material data sheets, especially if the manufacturer is new or little-known. Require test reports specifically for compression and creep. Conduct your own tests on a test bench before mass application on site. Spend a week testing so you don't waste a month troubleshooting.
Final summary for managers and chief engineers
The procedure for assembling flange connections in 2026 is not just a technical procedure. This is a strategic asset of the enterprise. Proper assembly reduces operating costs, improves safety, and extends equipment life.
What needs to be done right now?
- Conduct an audit of the current tool fleet and replace worn ones.
- Review the warehouse program: remove questionable gaskets and fasteners, paying special attention to the quality of the flanges themselves and their compliance with the stated standards.
- Train staff in new techniques, focusing on understanding the physics of the process rather than memorizing instructions.
- Implement a documentation system for each assembled unit.
Remember: the tightness of your production is maintained by tens of thousands of bolts. Each of them is important. Saving on build culture is a ticking time bomb that you may already hear ticking but ignore for the sake of the plan. Not worth it.
Technologies change, materials evolve, but the basic principle remains unchanged: respect for detail and attention to detail separates professionals from amateurs. In the conditions of Russian reality, where the safety margin is often tested by extreme temperatures and loads, this choice becomes a matter of business survival.